NIPPON CUTTING & WELDING EQUIPMENT CO., LTD.
SERVICES
Technology & Services
Heater / Non-Heater Regulator for Welding | Stable Pressure Control for Inert Gas and CO₂ Welding
Key Takeaways
• Heater / Non-Heater Regulators are designed to provide stable pressure and flow control for welding applications
• Support Argon, CO₂, and MAG gases for high-quality welding
• Heater-Type models reduce icing and pressure drop caused by gas expansion
• Suitable for general welding, continuous operation, and industrial production lines
ーーーーーーーーーーーーーーーーーーーーーーーーーーーーーーー
In welding processes that use inert gases or CO₂, the stability of pressure and flow is a key factor in determining weld quality. Unstable pressure can cause porosity and spatter, negatively affecting both the strength and appearance of welds.
Heater / Non-Heater Regulators for Welding are therefore developed to ensure precise pressure control, accommodating different welding process requirements.
In continuous CO₂ or MAG welding, rapid gas expansion often causes a significant temperature drop, leading to pressure loss and unstable flow. Using a suitable regulator especially a Heater-Type model helps mitigate these issues, enabling stable and uninterrupted welding operations.
Differences between Regulator Types
• Non-Heater Regulators are suitable for general welding applications or operations with relatively low flow rates
• Heater-Type Regulators include a heating system that prevents icing and pressure drop during continuous CO₂ / MAG welding
Both types maintain stable outlet pressure and help ensure consistent weld quality.
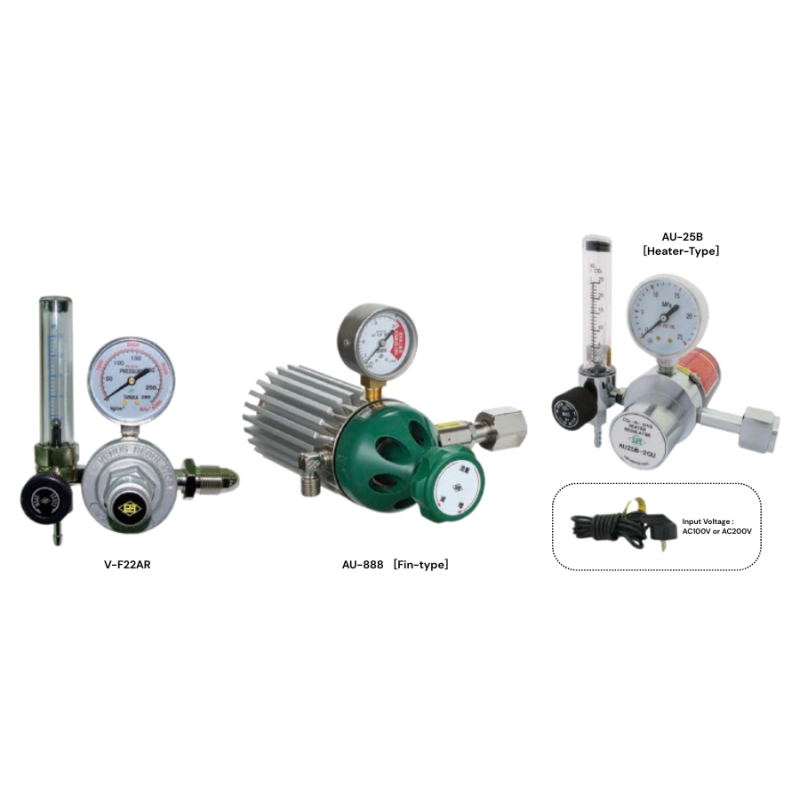
🔷 Models Specifications
• V-F22AR (Non-Heater Type)
Gas: Argon
Inlet pressure gauge: 25 MPa (Max. 15 MPa)
Maximum working pressure: 0.2 MPa (Preset)
Flow rate: 1–25 NL/min (P2 = 0.2 MPa)
Weight: 1.3 kg
• AU-888 (Fin-Type / Non-Heater)
Gas: CO₂ and MAG
Inlet pressure gauge: 25 MPa (Max. 15 MPa)
Maximum working pressure: 0.2 MPa (Preset)
Flow rate: 5–20 NL/min (P2 = 0.2 MPa)
Weight: 2.3 kg
• AU-25B (Heater-Type)
Gas: CO₂ and MAG
Inlet pressure gauge: 25 MPa (Max. 15 MPa)
Maximum working pressure: 0.25 MPa (Preset)
Flow rate: 1–25 NL/min (P2 = 0.25 MPa)
Weight: 1.9 kg
Industrial Applications
• TIG welding using Argon
• CO₂ / MAG welding in production lines
• Continuous welding processes requiring stable flow rates
• Factories seeking to reduce pressure drop and inconsistent weld quality
Selecting the appropriate Heater or Non-Heater Regulator according to the gas type and application ensures stable pressure and flow, reduces weld defects, and improves overall operational efficiency.
Summary
Heater / Non-Heater Regulators for Welding are essential components for controlling gas systems in welding applications. Choosing the right model for the gas type and operating conditions ensures consistent weld quality, enhanced safety, and reliable long-term performance.
ーーーーーーーーーーーーーーーーーーーーーーーーー
❓ FAQ
Q: When should a Heater-Type regulator be selected?
A: When performing continuous CO₂ / MAG welding or operating at high flow rates, where icing and pressure drop are likely to occur.
Q: For which applications is a Non-Heater regulator sufficient?
A: General welding tasks or operations with relatively low flow rates, while still maintaining stable pressure control.
Q: Does the regulator affect weld quality?
A: Yes. Stable pressure and flow directly reduce porosity and spatter, improving weld quality.
📚 Glossary (Key Terms)
• Regulator: A device that controls gas pressure and flow in welding applications
• Heater-Type Regulator: A regulator equipped with a heating system to reduce icing and pressure drop
• Non-Heater Regulator: A regulator without a heating system, suitable for general applications
• Porosity: Weld defects caused by unstable pressure or inconsistent gas flow
Company Information
Main 3 Products
Industrial gas pressure regulator / Gas cutting equipment
Phone Number
With 36 years of experience in Thailand, NIPPON CUTTING & WELDING EQUIPMENT CO., LTD. has continued to manufacture related equipment based on gas cutting technology. In recent years, in addition to pl ...
CATALOG
Related Catalogs
PICKUP
Technology & Services
CONTACT
Contact